Skip to content

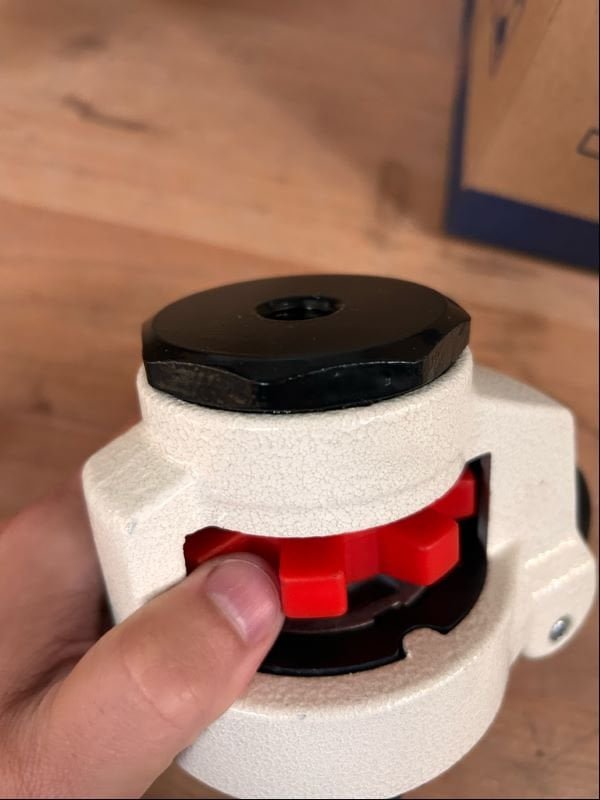
At assembly, a levelling castor may fail without dramatic breakage. A stem may bind, or the adjustment may feel rough even though the castor looks acceptable in its packaging.
Buyers should inspect a levelling castor in four stages: check the top plate, housing, wheel, and packaging for damage; confirm the M16 thread accepts the supplied stem smoothly; operate the levelling mechanism without abnormal resistance; and record results before the lot enters assembly.
That is why arrival inspection should move from appearance to function. In one customer case, supplied stems stopped after one or two turns where paint had entered the internal thread, while clean threads accepted full insertion. Buyers should therefore verify function before assembly, not just appearance.
Why Can a Levelling Castor Look Acceptable but Fail at Assembly?
A castor can look complete while a functional interface is contaminated or out of tolerance.
The short answer is that appearance does not prove thread fit, movement, or adjustment function.
Paint, powder, debris, burrs, or damage at the entrance of an internal thread can stop a matching stem before the required engagement. The top plate may still look uniform, and the housing and wheel may appear undamaged. Industrial coating guidance therefore treats threaded holes as areas that often need masking, not merely cosmetic surfaces.[1]
During receiving inspection, a part that needs cleaning before the stem can fit is not equivalent to a clean part passing the agreed check. A buyer should separate four questions: Does the castor look intact? Does the thread fit? Do the moving parts work? Can the result be recorded against the delivery?
How Can Buyers Check the Thread Before Fitting the Castor?
Thread fit is easy to overlook because a quick visual check cannot reveal the full condition of the thread.
Use the correct supplied M16 stem or an agreed thread gauge, turn it by hand, and confirm smooth engagement to the agreed seating or engagement point.
First, look into the opening for paint, chips, burrs, or foreign material. Do not force the stem with a spanner. If it stops unusually early, binds, or feels different from a known-good sample, place the unit on hold and record the observation. A go/no-go gauge can provide a repeatable limit check when the thread class and acceptance standard are defined.[2]
The supplied stem is valuable because it tests the actual mating condition used in the application. Define whether the check is 100% or sample-based, identify the lot, and state the pass/fail condition. A thread-chasing tool may restore a part, but it should not replace supplier process control or hide an incoming nonconformance.
What Other Damage Should Buyers Look for on Arrival?
Thread fit is only one part of an arrival inspection. Packaging damage or a bent component can create a different failure even when the stem enters smoothly.
Compare the delivery with the approved sample, drawing, or purchase specification. Check the top plate, housing, wheel, mounting interface, supplied hardware, and packaging.
Look for a bent top plate, cracked or deformed housing parts, chipped coating at functional edges, wheel damage, unusual looseness, missing nuts or stems, and compression or impact marks from transport. Keep cosmetic findings separate from functional findings. A colour variation may need a cosmetic decision, while a damaged mounting face or restricted thread can prevent assembly.
Confirm supplied parts match the order and remain traceable to the delivery lot. If a finding could affect fit or movement, photograph and isolate it, then compare it with the acceptance criteria. Incoming inspection can combine visual, thread, burr, depth, and functional-fit checks for threaded features.[3]
How Can Buyers Confirm That the Levelling Mechanism Works?
A castor can pass a visual inspection and thread check yet still be difficult to adjust or unable to reach the required position.
Assemble the supplied stem and related hardware as intended. Operate the levelling mechanism by hand through its normal range and check for smooth movement, abnormal resistance, incomplete engagement, or unusual play.
Perform the check on a stable surface and compare it with an approved sample or agreed functional description. Confirm that adjustment does not require forcing the thread and that the castor reaches the intended contact position. If a defined load matters, agree the load, surface, and measurement method separately. A hand check does not prove catalogue load capacity or long-term service performance.
Record the result as a functional observation. The buyer confirms assembly and adjustment; application validation still depends on specified load, surface, and working conditions.
Accept the castor only after visual, thread-fit, and levelling-function checks pass, with the result recorded against the delivery lot and agreed acceptance criteria.
References
- PCI Magazine, Powder Coating Masking Fundamentals.
- Higher Precision, GO/NO-GO Thread Gages: Plug vs. Ring & How to Use Them.
- Neway Precision, How are zinc die cast components inspected before shipment?.